Engineered for ultra-fast beverage filling lines, high-pressure carbonated soft drinks, and airtight food-grade preservation.







Understanding the Metallurgical and Geometric Benchmarks of Modern Beverage End Packaging
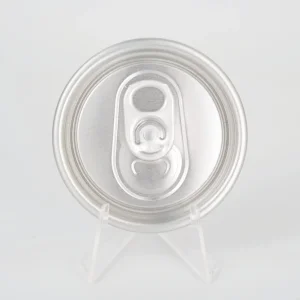
In the high-speed global beverage canning industry, the transition toward lightweighting without sacrificing structural integrity represents the ultimate engineering milestone. As a premier Wholesale SOT 200 B64 Manufacturer & Supplier, our technical framework centers around the high-precision 200 diameter (50mm nominal aperture) Stay-On Tab (SOT) end featuring the optimized B64 profile geometry. Designed specifically to interface seamlessly with modern sleek, slim, and standard aluminum beverage body profiles, the SOT 200 B64 represents a benchmark in metal conservation, pressure holding capacity, and double-seam compatibility.
The engineering topology of the SOT 200 B64 end is fabricated utilizing high-tensile AA5182-H48 aluminum-magnesium alloy for the end shell stock, combined with AA5052-H19 alloy for the pull tab mechanism. By optimizing the score-line residual metal thickness down to 32 ± 3 microns, our high-speed stamping presses achieve an ideal operational harmony: exceptional pop-and-pull ergonomic performance paired with an explosive burst threshold exceeding 6.2 bar (90 psi). This satisfies the rigorous thermal and mechanical stress profiles imposed by carbonated soft drinks (CSD), craft beer pasteurization, nitrogen-dosed energy beverages, and tunnel pasteurization processes.
| Parameter Benchmark | SOT 200 B64 (Optimized) | Standard SOT 202 Profile | Traditional 206 Profile | CDL High-Pressure Profile |
|---|---|---|---|---|
| Nominal Diameter | 50.8 mm (200#) | 54.0 mm (202#) | 59.0 mm (206#) | 50.8 mm (200#) |
| Shell Metallurgy | AA5182-H48 High-Magnesium | AA5182-H39 / H48 | AA5052 / AA5182 | AA5182-H48 Ultra-Thin |
| Buckle Pressure Rating | ≥ 6.2 Bar (90 PSI) | ≥ 5.8 Bar (84 PSI) | ≥ 4.5 Bar (65 PSI) | ≥ 6.5 Bar (94 PSI) |
| Internal Coating System | BPA-NI Organosol / Acrylic | Epoxy Ester / BPA-NI | Standard Epoxy | Gen-3 BPA-NI Polymer |
| Seamer Line Speed Capability | Up to 1,500 CPM | Up to 1,200 CPM | Up to 800 CPM | Up to 1,600 CPM |
| Metal Mass Savings | 12.5% vs 202 Standard | Baseline Reference | -22% (Heavier) | 14.0% vs 202 Standard |
Pioneering Next-Gen Down-Gauging, Non-BPA Barrier Chemistries, and Smart Supply Systems
Iterating metal thickness from 0.220mm down to 0.203mm utilizing finite element analysis (FEA) countersink optimization, reducing carbon footprint while guaranteeing structural buckle resistance under high pressure.
Pioneering advanced water-based polyester and acrylic organosol spray liners that eliminate Bisphenol A (BPA-NI) and vinyl compounds, ensuring 100% regulatory alignment with EU REACH and US FDA food contact rules.
Deploying sub-second high-precision laser etching underneath the SOT tab mechanism. This enables brand owners to offer digital promotional codes, direct anti-counterfeiting verification, and supply chain track-and-traceability.
Tailored Engineering Parameters Across Diverse Global Beverage and Food Segments
Carbonated beverages impose continuous internal expansion pressures up to 4.5 volumes of CO₂. The B64 profile countersink depth and modified bead configuration prevent dome reversal or pinhole stress corrosion cracking during prolonged tropical warehousing. The compound lining gasket is formulated with micro-cellular PVC-free plastisol, maintaining an airtight hermetic seal across temperature fluctuations from -2°C to 50°C.
Tunnel pasteurization subjects beverage ends to extreme thermal shocks (60°C–68°C for 20+ minutes) alongside internal pressure spikes. Our SOT 200 B64 design incorporates engineered shell temper curves that absorb thermal expansion while eliminating permanent metal deformation, protecting double-seam integrity on high-speed Angelus, Ferrum, or Krones seamers.
High acidity (pH < 2.8) and volatile vitamin/mineral fortifiers in functional beverages demand non-reactive interior liners. Our dual-coat acrylic and modified organosol barrier lacquers undergo 100% online Enamel Rater inspection (< 2.0 mA porosity threshold), preventing copper/iron ion leaching and preserving shelf flavor stability up to 24 months.
Extending beyond liquid applications, customized 200# and 206# easy-open lids provide vacuum retention and moisture-free barrier protection for premium milk powders, infant formula, coffee grounds, and nutraceutical products under vacuum or nitrogen-flush packaging conditions.
Integrating Automated Stolle Conversion Presses, High-Speed Vision AI, and Port-Adjacent Logistics
Our centralized manufacturing infrastructure in Shanghai leverages China’s advanced Industrial 4.0 ecosystem. By combining high-speed automated multi-die conversion presses (such as Stolle and Minister systems operating at speeds exceeding 3,000 ends per minute) with real-time optoelectronic inspection arrays, we deliver world-class consistency at wholesale volume economies.
Long-term strategic coil hedging with Tier-1 aluminum mills (Chinalco, Southwest Aluminum) ensures certified AA5182/AA3104 alloy purity, exact thickness tolerances (±0.002mm), and stable raw material pricing for contract buyers.
High-resolution 360-degree inline vision cameras inspect 100% of manufactured ends for score scratches, tab misalignment, compound placement voids, or curling edge deformities, auto-ejecting non-conforming units instantaneously.
Ends are packed in anti-static polyethylene sleeves, sealed in corrugated fiber drums with desiccants, and robotically palletized with top frames and stretch-hood wrap, maximizing container loading density while resisting maritime humidity.
Seamless International Logistics, Regulatory Certification, and Technical On-Site Seamer Calibration
Procuring metal packaging at global scale requires absolute regulatory safety and flawless technical compatibility. Our international engineering desk provides full end-to-end support for global enterprise procurement managers, offering clear technical documentation, compliance declarations, and line-matching analysis before high-volume commercial production.
Every production lot is issued with full analytical testing reports: FDA 21 CFR 175.300 food contact compliance, EU Regulation 1935/2004 migration tests, heavy metal limits (RoHS/REACH), and GB 4806.10 certification. Complete traceability connects finished pallet barcodes back to raw coil mill heat numbers.
Our packaging engineers supply custom seamer chuck and roll profile drawings (compatible with Ferrum, Angelus, Continental, and Krones equipment). We deliver trial sample lots for double-seam teardown evaluation, thickness crossover verification, and optical seam projector profiling.
While high-speed custom printed aluminum cans typically require minimum runs of 100,000 units due to dry-offset plate setup, standard plain B64 ends, SOT 202/200 ends, and stock coil rolls ship in flexible trial quantities starting from 200,000 pieces within 15 working days.
By combining lightweighted B64 profile geometry with ocean-freight container cube optimization, we help enterprise purchasing directors reduce freight-per-thousand-ends by up to 14%, while minimizing seamer downtime through uniform metal hardness profiles.
Factory-Direct Aluminum Beverage Cans, Tinplate Lids, and Precision Aluminum Coils






Expert Answers on Metallurgy, Seaming Compatibility, Quality Assurance, and Logistics
