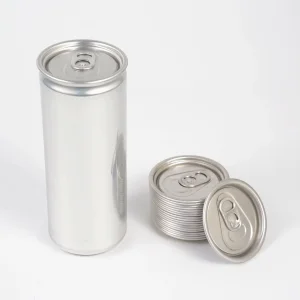
The global metal beverage packaging landscape is undergoing a structural transformation driven by decarbonization mandates, consumer preferences for premiumization, and the rapid growth of craft beverage ecosystems. Modern consumers no longer perceive the aluminum beer can purely as a functional vessel; rather, it serves as an interactive canvas for brand storytelling, tactile engagement, and eco-friendly consumerism. According to global packaging intelligence metrics, aluminum beverage can demand is projected to reach over 630 billion units annually, with personalized and custom-decorated segments outpacing commodity growth by a margin of 2.4x.
Aluminum represents a closed-loop infinite material. Recycling aluminum saves up to 95% of the energy required for primary refining, positioning personalized cans as the preferred sustainable choice over PET and glass.
Transitioning from traditional shrink-sleeves to direct-to-can digital HD printing eliminates non-recyclable polymer layers while enabling ultra-short run personalization for craft microbreweries.
Advanced Drawn and Wall Ironed (DWI) technologies utilize high-performance 3104-H19 aluminum alloy coils to reduce container weight by 14% while retaining structural axial strength up to 850N.
Historically, high-volume dry offset lithography required minimum order quantities (MOQs) exceeding 100,000 units per artwork SKU, creating high barriers to entry for seasonal craft beers, experimental IPAs, and localized co-packing events. The integration of high-speed industrial ink-jet digital printing and variable datamapping technology now allows global beverage enterprises to run personalized packaging runs with variable QR codes, localized geographical art, and tactile matte-gloss finishes down to micro-batches of 5,000 units without sacrificing operational line speed.
Information Gain Insight: Modern personalized beer packaging eliminates single-use plastic labels. By replacing pressure-sensitive labels (PSL) with direct-to-can UV curable varnishes, brands achieve immediate compliance with European Green Deal Packaging and Packaging Waste Regulation (PPWR) mandates.
To capture maximum search intent depth, enterprise procurement strategies for wholesale personalized beer cans are divided into three primary buyer personas: Large-scale Multinational Beverage Conglomerates, Regional Contract Packers (Co-packers), and Boutique Craft Breweries. Sourcing decisions are no longer made purely on unit price; instead, decision-makers analyze Total Cost of Ownership (TCO), Overall Equipment Effectiveness (OEE) on filling lines, double-seam tolerance, and coating compliance.
| Procurement Metric | Multinational Breweries | Contract Co-Packers | Craft & Specialty Brands |
|---|---|---|---|
| Primary Sourcing Focus | High-speed line efficiency, axial load stability | Dimensional flexibility, multi-neck compatibility | Low MOQs, high-fidelity tactile finishes |
| Alloy Requirement | 3104-H19 Body / 5182-H48 End Shell | 3104-H19 Standard / Custom 202 SOT | 3104-H19 Thin-gauge / 200 Sleek Formats |
| Coating & Compliance | BPA-NI (Non-Intent) & Epoxy Acrylic | Universal organosol for multi-beverage pH | BPA-NI, high-acid craft beer resistant |
| Key Supply Risk | Supply chain disruption, ocean freight delay | Plate setup lead times, SKU switching loss | High inventory holding costs, design errors |
When procuring personalized aluminum beer cans globally, filling line efficiency depends on precision necking and flange geometry. A variation of merely 0.05mm in flange width can cause seaming chuck slippage, leading to micro-leaks, oxygen ingress, and loss of carbonation ($CO_2$ pressure degradation). Premier suppliers utilize fully automated vision inspection systems capable of detecting 100% of body dents, pinholes down to 0.02mm, and flange deformities prior to palletization.
Furthermore, internal corrosion protection is critical for preserving beer organoleptic profile. Craft beers featuring elevated hops profiles, acidic fruit adjuncts, or sour strains display aggressive low pH values (3.2 – 3.8). Modern manufacturing applies advanced water-based BPA-NI internal lacquers, applied via electrostatically assisted spray guns to guarantee complete internal coverage (35 – 50 mg/sqm film weight), eliminating metal taste transfer and extending shelf life up to 18 months.
China’s metal packaging infrastructure has evolved from labor-intensive processing to fully integrated Industry 4.0 smart manufacturing complexes. Shanghai and regional industrial clusters combine raw aluminum ingot refining, precision cold-rolling coil production, high-speed cupping, deep-drawing, and automated warehousing within unified industrial corridors. This vertical integration provides unmatched cost efficiency, agility, and supply chain resilience against global market fluctuations.
Modern Chinese facilities utilize ultra-high-speed multi-die cupping presses capable of processing up to 3,000 aluminum cups per minute. Wall ironers sequentially reduce body thickness down to sub-millimeter tolerances while maintaining consistent grain alignment in the 3104-H19 alloy matrix, maximizing burst pressure resistance up to 6.2 bar.
Zero-defect manufacturing protocols incorporate continuous online high-voltage porosity testers (Enamel Rater Inspection). By passing a low-amp electrical current through filled electrolyte solutions inside coated cans, automated systems detect micro-flaws in internal lacquers in real-time (< 2mA threshold), automatically rejecting defective units.
Supply chain resilience relies heavily on export packaging density and sea-freight durability. Wholesale empty aluminum cans represent lightweight but voluminous freight. Advanced packing facilities employ high-density automated bulk palletizers, utilizing moisture-resistant solid kraft separator sheets, top wooden frames, and heavy-duty 5-layer stretch-hood wrapping. This setup allows up to 120,000 standard 330ml cans or up to 700,000 202# Easy-Open Ends (SOT/RPT) to be safely packed into a standard 40ft High Cube (HQ) ocean container, reducing landed transport costs per unit by up to 18%.
To assist procurement officers in conducting rigorous life-cycle assessments (LCA), the following matrix analyzes the physical, financial, and environmental performance of aluminum beverage cans compared against traditional glass bottles and polyethylene terephthalate (PET) containers across global supply chains.
| Performance Parameter | Aluminum Can (DWI) | Glass Bottle (Returnable/One-Way) | PET Plastic Container |
|---|---|---|---|
| Tare Weight Ratio (Empty vs Fill) | ~1:25 (Ultra-Light) | ~1:1.8 (Heavy Freight Burden) | ~1:20 (Lightweight) |
| UV Light & Oxygen Barrier | 100% Absolute Barrier | Partial Barrier (UV sensitive) | Permeable ($O_2$ ingress over time) |
| Thermal Conductivity (Chill Speed) | Rapid (High Conductivity) | Slow (Insulating glass wall) | Moderate |
| Breakage Loss in Logistics | < 0.01% (Ductile Metal) | up to 2.5% (Brittle Fracture) | < 0.1% (Deformation) |
| Real Recycled Material Rate | ~70% Closed-Loop | ~35% (Regional dependency) | < 15% (High degradation) |
While raw material unit costs for aluminum fluctuated historically, the combined freight savings, reduction in cooling energy requirements, zero breakage claims, and high filling speeds (up to 90,000 cans/hour on automated rotary filling lines) position personalized aluminum cans as the most cost-effective packaging medium over long-distance logistics corridors.
Standard packaging specs cannot address the full spectrum of modern beverage chemistry. Advanced manufacturing customizes can geometries, alloy tempers, and lid configurations to suit specific regional and chemical applications.
Nitrogenated beers and cold-brew coffees require specialized internal liquid nitrogen injection dosing prior to seaming. Personalized 330ml Sleek and 500ml Standard cans are engineered with internal sidewall pressure tolerances up to 6.2 bar to support in-can nitrogen widgets, producing a creamy draught-style head upon opening.
Premixed spirits, hard seltzers, and wine-based RTDs demand high corrosion resistance due to elevated alcohol by volume (ABV up to 15%) and organic acid combinations. Enhanced cross-linked epoxy or organosol internal lacquers prevent flavor degradation and preserve brand integrity.
Exporting sensitive infant formula, nutritional powders, or coffee beans to tropical or coastal markets requires rust-proof 401# and 502# Easy-Open Lids featuring tinplate or aluminum barrier shells with high salt-spray resistance (> 96 hours neutral salt spray testing without oxidation).
Canned coffee, milk-based teas, and wet pet food undergo aggressive thermal retort processing at temperatures reaching 121°C (250°F) for up to 45 minutes. Lids and can bodies are engineered with specialized thermal-stable compound gaskets to prevent seal collapse during pressure equalization cycles.
Direct insights from our packaging application engineers regarding common manufacturing, seaming, compliance, and custom ordering questions.