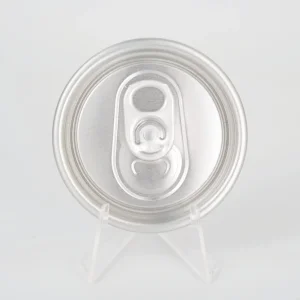
Precision-engineered aluminum easy-open ends, lids, coils, and containers optimized for high-speed filling lines and extended product freshness.







Analyzing the pivotal shift from conventional single-use rigid plastics to high-barrier, infinitely recyclable metal food storage ecosystems.
The global food packaging domain is experiencing a structural migration toward non-reactive, high-barrier metallic substrates. Driven by stringent international mandates—such as the European Union’s Packaging and Packaging Waste Regulation (PPWR) and US FDA environmental initiatives—food manufacturers are accelerating the phase-out of multi-layer polymer laminates. As a premier global leading aluminum food storage supplier, China’s advanced packaging manufacturing hubs deliver structural aluminum alloys (3104-H19, 5182-H48, 8011-O) that achieve complete circularity without material degradation.
Food degradation is predominantly driven by photo-oxidation, moisture ingress, and volatile organic compound (VOC) cross-contamination. High-performance aluminum easy-open lids (EOE), metal can bodies, and lacquered coils provide a absolute physical barrier with zero Oxygen Transmission Rate (OTR) and zero Water Vapor Transmission Rate (WVTR). This structural advantage extends product shelf life up to 36 months under adverse tropical or freeze-thaw environmental storage conditions.
Comprehensive technical benchmarks detailing alloy composition, BPA-NI organosol chemistry, and double-seam double-seam mechanics.
| Component Application | Alloy Grade & Temper | Tensile Strength (MPa) | Yield Strength (MPa) | Internal Lining Technology | Primary Regulatory Compliance |
|---|---|---|---|---|---|
| Can Body (DWI / DRD) | AA 3104-H19 | 270 – 310 | 240 – 280 | BPA-NI Modified Acrylic / Polyester | FDA 21 CFR 175.300, EU 10/2011 |
| Easy-Open End (EOE Shell) | AA 5182-H48 | 360 – 400 | 310 – 350 | High-Elasticity Vinyl Organosol | GB 4806.10-2016, LFGB § 30/31 |
| Pull Tab Mechanism | AA 5052-H38 | 210 – 250 | 160 – 200 | Clear Anodized / Epoxy Lacquer | RoHS 2011/65/EU, REACH SVHC |
| Closure Foil Stock | AA 8011-O / H18 | 140 – 180 | 110 – 150 | Heat-Sealable Polyolefin/PE Coating | ISO 22000, US CPG Sec. 545.400 |
Our factory deploys advanced Non-Intent Bisphenol A (BPA-NI) polymeric spray lacquers. Specially formulated for high-acid food products (pH < 3.5) and aggressive sulfur-bearing protein items, these inner coatings prevent iron ion migration, eliminating metallic off-flavors and ensuring 100% organoleptic purity.
Forming the score-line on 200#, 202#, 307#, and 401# easy-open lids demands sub-micron tooling precision. We maintain score residual tolerances within ±2 microns. This guarantees an ultra-smooth opening force (< 30 N pop, < 50 N tear) while maintaining minimum pop-and-burst thresholds up to 6.2 bar for pressurized contents.
Designed for universal compatibility with high-speed automatic seamers (Angelus, Ferrum, Consolidated Can). Our lid radius curl profile, countersink depth, and compound lining weight achieve tight overlap percentages (> 55%) and seam tightness (> 85%), completely eliminating micro-leakage risks during vacuum sealing.
Unrivaled vertical integration from raw aluminum ingot processing to high-speed automated stamping and global containerized shipping.
Our state-of-the-art Chinese manufacturing complex houses multiple high-speed stamping presses from industry leaders like Minster and Stolle, capable of operating at speeds up to 3,000 ends per minute per line. Backed by fully integrated coil slitting, lacquer coating, and optical machine vision inspection units, our factory ensures continuous output with zero defect tolerance.
Tailored packaging engineering adapted for regional market requirements, processing methods, and regulatory frameworks.
Specific Challenge: Powdered milk, bio-active protein isolates, and clinical nutritional formulas require absolute zero-oxygen environments to prevent lipid oxidation, rancidity, and moisture clumping.
Engineered Solution: Implementation of 401# and 502# peel-off foil membranes and aluminum easy-open lids featuring gas-flush channels. Supports modified atmosphere packaging (MAP) with nitrogen flushing, maintaining internal residual oxygen levels below 0.5% throughout a 36-month shelf life.
Specific Challenge: Frozen seafood, cold-stored produce, and specialized biochemical foods stored at -40°C suffer from thermal shock embrittlement, causing score-line micro-fissures in standard packaging.
Engineered Solution: Freeze-resistant 209# aluminum lids made from high-ductility AA 5182 alloy with cryogenic organosol linings. Retains elasticity down to -50°C without micro-fracturing or seal degradation during rapid thaw cycles.
Specific Challenge: Craft beers, sparkling waters, and hard seltzers exert internal pressures up to 5.5 bar during flash pasteurization (up to 68°C).
Engineered Solution: 202# SOT (Stay-On Tab) and 200# RPT (Resealable Pull Tab) easy-open lids calibrated for 6.2+ bar burst resistance, featuring thick-gauge 5052 tabs to eliminate tab deformation during high-speed consumer opening.
Specific Challenge: Canned meats, fish, soups, and ready-to-eat meals undergo intensive retort cooking cycles (121°C to 135°C for 30–60 minutes), creating severe thermal expansion stress.
Engineered Solution: Retort-grade 307# and 603# food-grade tinplate and aluminum lids with heat-stabilized, high-crosslink epoxy liners, ensuring zero delamination, blistering, or rust formation post-autoclave treatment.
Strategic technology initiatives driving ultra-lightweighting, digital traceability, and carbon-neutral packaging manufacturing.
By optimizing shell profile geometries and leveraging work-hardened AA 5182-H49 alloys, our R&D engineering team is reducing lid metal thickness from 0.22mm down to 0.18mm without sacrificing structural buckle resistance. This initiative yields a 12% net reduction in carbon footprint per million units.
Integration of high-speed inline laser engraving on pull tabs and end shells. Enables 2D DataMatrix and QR code printing for real-time supply chain origin tracking, anti-counterfeiting verification for premium milk powders, and direct consumer engagement.
Advancing raw material integration to utilize up to 80% Post-Consumer Recycled (PCR) aluminum coil stock. Recyclable metal packaging uses 95% less energy than primary aluminum smelting, directly helping brand owners reach Scope 3 ESG targets.
Explore our specialized range of high-barrier aluminum cans, sterilizable lids, and industrial tinplate packaging solutions.








Demonstrating rigorous testing protocols, international certifications, and local technical assistance networks.
Our manufacturing sites adhere strictly to globally recognized quality standards. Comprehensive laboratory documentation accompanies every shipment to facilitate seamless customs clearance across European, North American, APAC, and Middle Eastern entry ports.
Every manufacturing batch undergoes destructive and non-destructive laboratory testing prior to release:
Addressing engineering specifications, minimum order requirements, and line integration parameters for international procurement teams.