Engineered for automated high-speed canning lines, powder processing plants, and food-grade barrier preservation.
In the rapidly transforming landscape of global fast-moving consumer goods (FMCG), pharmaceuticals, and industrial chemical storage, the demand for high-quality global leading alfoil containers manufacturers products has escalated from basic containment needs to sophisticated, multi-layer barrier engineering. Aluminum foil (alfoil) containers, easy-open ends (EOE), and continuous coil alloys represent the pinnacle of sustainable, hermetic, and lightweight packaging solutions. Modern FMCG brand owners and industrial procurement leadership face increasing pressures to balance strict decarbonization mandates with uncompromised organoleptic protection, shelf-life extension, and high-speed filling line performance.
This technical whitepaper synthesizes deep empirical data, metallurgical breakthroughs, and regulatory frameworks governing global aluminum container manufacturing. Through precise alloy selection—such as 3104-H19 for deep-drawn can bodies, 5182-H48 for high-buckle easy-open ends, and 8011/5052 lacquered coils for hermetic closures—leading global manufacturers are redefining the operational limits of metal packaging. The purpose of this guide is to empower supply chain executives, packaging engineers, and enterprise buyers with actionable engineering insights, total cost of ownership (TCO) benchmarks, and regulatory compliance roadmaps.
Key Insight for Enterprise Procurement: Modern aluminum container engineering has shifted from standard gauge thickness reduction to advanced metallurgical grain refinement and organic barrier lacquers (BPA-NI). Achieving zero pinholes at 0.015mm foil gauges while guaranteeing double-seam integrity under 121°C retort conditions requires exact thermal temper control and state-of-the-art vision inspection systems.
Four core structural shifts driving technical specifications across international supply chains through 2030.
Global regulatory bodies, including the European Union (PPWR) and US State EPA mandates, are enforcing strict circular economy targets. Aluminum stands unique as an infinitely recyclable element without property degradation. Over 75% of all aluminum ever produced remains in productive use today. Leading manufacturers are integrating high recycled content (post-consumer scrap) into 3104 and 5182 ingot formulations, dropping carbon footprints by up to 95% compared to primary smelter extraction without sacrificing tensile or yield strength.
Driven by rising freight costs and carbon reduction goals, world-class aluminum container plants utilize advanced cold-rolling mill technologies to achieve down-gauging. Body stock thickness for beverage cans has dropped toward 0.24mm-0.26mm, while container foil sheets maintain micro-gauge tolerances (+/- 0.002mm). Maintaining structural column collapse resistance and internal burst strength at these lightweight limits requires highly homogenized alloy microstructures and precise temper specifications (H19, H48, H18).
Global compliance frameworks, including EU Commission regulations and California Proposition 65, have accelerated the absolute phasedown of Bisphenol-A (BPA) internal coatings. Premium manufacturers now employ BPA-Non-Intent (BPA-NI) acrylic, polyester, or organosol liquid and powder linings. These engineered polymer matrices prevent flavor scalping, resist aggressive low-pH acidic beverages (e.g., energy drinks, craft beers), and eliminate metal ion leaching into sensitive dairy or infant powders.
In high-speed processing facilities running at speeds over 1,500 units per minute, container dimensional consistency is critical. Modern alfoil container manufacturers integrate high-resolution 4K optical camera inspection systems right on the press lines. These automated vision sensors identify surface pinholes, flange dents, and curl deviations in real time, guaranteeing seamlessly uniform feeding into customer automated filling, seaming, and retort heat-sealing machinery.
Quantitative standards enterprise buyers must evaluate when vetting global tier-1 aluminum packaging factories.
Purchasing enterprise aluminum containers or raw coil stock requires rigorous technical verification. A primary cause of line jams, product spoilage, or premature corrosion in commercial packaging stems from non-conforming grain structure or sub-standard coating weight. Below is a comprehensive engineering benchmark matrix employed by leading international QA teams:
| Testing Parameter | Standard Test Method | Target Engineering Specification | Impact on Product Performance |
|---|---|---|---|
| Enamel Conductivity (Enamel Rater) | WACO Conductivity Tester (1% NaCl solution) | < 0.05 mA (Standard), < 0.01 mA (Critical Foods) | Prevents pinhole pin-pointing, metal reaction, and off-flavor migration over 24-month shelf life. |
| EOE Buckle Strength | Pneumatic/Hydraulic Pressure Chamber | > 6.2 bar (202 SOT / RPT ends) | Guarantees lid retention during high-temperature thermal processing and internal carbonation pressure. |
| Double Seam Geometry | Optical Seam Saw & Video Metrology | Overlap % > 80%, Seam Tightness > 85% | Eliminates micro-leakage and bacterial ingress in wet canning and sterile dry powder applications. |
| Coating Weight & Thickness | Solvent Extraction / XRF Gauge | Internal: 6–12 g/m²; External: 3–5 g/m² | Ensures complete chemical barrier coverage while retaining flexibility during die-forming. |
| Alloy Grain Earing Rate | Tensile / Deep Draw Testing | Earing ratio < 2.0% (3104-H19 Coil) | Prevents uneven rim trimming and flange tears in deep-drawn smooth-wall alfoil containers. |
Engineered alloy formulations and lid configurations configured for distinct product chemical profiles.
Nutritional powders are highly vulnerable to moisture ingress and oxygen-induced fat oxidation. High-quality aluminum easy-open ends (such as 401# and 502# sizes) feature peelable foil membranes or high-barrier aluminum shells. Paired with nitrogen flushing protocols, these containers maintain headspace oxygen below 0.5%, preserving active vitamins and essential fatty acids over extended shelf cycles.
For wet food products requiring autoclave steam sterilization (up to 121°C for 45 minutes), heavy-gauge smooth-wall alfoil containers and tinplate/aluminum lids provide structural rigidity. The cross-linked polymer lacquers prevent sulfur staining from meat proteins and withstand thermal expansion stress without seal delamination or micro-channeling.
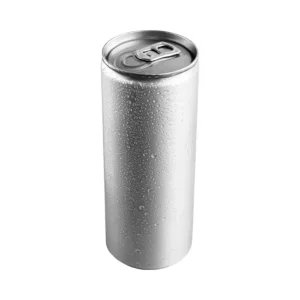
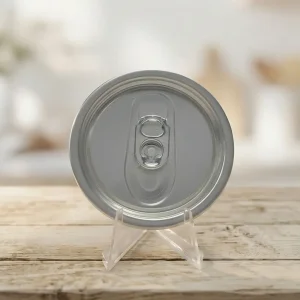
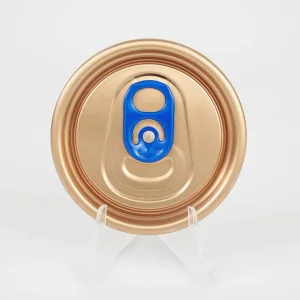
Beverage filling lines running at speeds of up to 2,000 cans per minute require dimensional accuracy in 200#, 202#, and 206# Stay-On-Tab (SOT) and Ring-Pull-Tab (RPT) ends. Paired with 3104-H19 two-piece aluminum cans in 200ml, 330ml, 355ml (12oz), and 473ml (16oz) formats, these systems maintain up to 4.2 volumes of CO2 or liquid nitrogen dose pressure.
Specialty chemical powders and electronic-grade reagents demand complete static dissipation and moisture shielding. Anti-static 300# aluminum easy-open ends and rigid heavy-wall containers prevent volatile organic compound (VOC) escape, ambient moisture absorption, and combustion risks induced by triboelectric charge generation during transportation.
Navigating complex international market entry standards with fully certified manufacturing protocols.
Exporting food-contact metal packaging across North America, the European Union, the Middle East, and Asia-Pacific requires comprehensive regulatory dossiers. Leading Chinese factories operating at global scale enforce full alignment with international food contact materials (FCM) regulations, giving importers and brand owners total legal safety.
Resinous and polymeric coatings utilized on all internal container surfaces are rigorously tested under US FDA 21 CFR 175.300 standards for total extractives in water, heptane, and alcohol stimulants, guaranteeing zero toxicological release under high-temperature processing.
Compliance with Good Manufacturing Practice (GMP) EC 2023/2006 and European Framework Regulation 1935/2004 ensures overall migration limits (OML) and specific migration limits (SML) are systematically logged via third-party laboratories (SGS, Intertek, TÜV Rheinland).
Manufacturing facilities operate under hazard-free HACCP and BRCGS Global Standard for Packaging Materials certification. Automatic air wash systems, optical defect sorting, and positive pressure cleanroom zones eliminate physical and biological contamination risks.
Logistics & Customs Safeguards: High-volume global shipments are backed by localized technical service engineers who assist client plants during initial double-seam set-up, seamer chuck alignment, and line speed optimization, ensuring seamless transition from dock to processing floor.
Pioneering the next era of high-barrier, zero-carbon aluminum container manufacturing technology.
Deployment of bio-based, plant-derived monomer internal coatings achieving equal chemical resistance as synthetic lacquers while drastically cutting embodied carbon.
Advanced ultra-thin foil container stamping utilizing servo-electric presses with nanometer die gap control, reducing container raw material mass by an additional 8%.
Near-Infrared (NIR) and laser-induced breakdown spectroscopy (LIBS) scrap sorting in manufacturing facilities to achieve 98%+ closed-loop alloy segregation.
Full commercial supply of 100% green-hydrogen smelted aluminum containers, offering world-first net-zero carbon packaging footprints for enterprise FMCG clients.
Direct answers from senior packaging metallurgists and quality control directors.
High-precision aluminum cans, easy-open ends, and specialized lids ready for global export logistics.