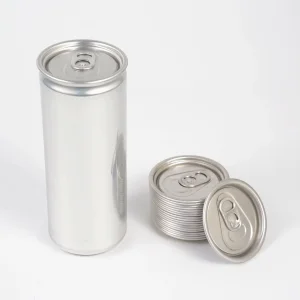
Explore our primary tier of engineered tinplate closures, ultra-lightweight beverage cans, and high-integrity sealing technology designed to integrate seamlessly into high-speed automated canning lines worldwide.







The global rigid packaging ecosystem is undergoing an unprecedented paradigm shift. Driven by worldwide decarbonization mandates, Extended Producer Responsibility (EPR) regulations, and shifting consumer sentiment away from single-use plastics (PET), the 330ml aluminum beverage can has solidified its dominance as the international benchmark format. Operating at the intersection of material science, industrial automation, and circular logistics, modern 330ml aluminum containers offer unmatched barrier performance, supply chain efficiency, and brand equity.
From an economic standpoint, the 330ml form factor represents the optimal balance between volumetric fill speed, stackability, and shipping weight. Freight logistics favor metal containers due to their high spatial efficiency—allowing up to 40% more liquid volume per pallet compared to traditional glass bottles. Furthermore, the inherent thermal conductivity of AA3104 alloy enables rapid chill-down cycles in commercial refrigeration, significantly reducing retail energy footprint.
Zero oxygen transmission rate (OTR) and complete light blocking shield sensitive compounds from photo-degradation and oxidative rancidity, extending shelf life beyond 18 months.
High structural strength-to-weight ratio minimizes secondary outer packaging needs, cutting gross shipping mass and maximizing sea container payload utilization.
Utilizing post-consumer recycled (PCR) aluminum stock reduces carbon intensity from ~12 kg CO2e/kg primary metal down to under 1.5 kg CO2e/kg closed-loop metal.
A standard 330ml aluminum can is an engineering marvel produced via the Draw and Wall Ironing (DWI) process. The container body is manufactured using high-formability AA3104-H19 aluminum alloy, characterized by precise manganese and magnesium content that imparts superior strain-hardening properties during deep drawing. The can top end employs AA5182-H48 alloy, formulated for high tensile strength to withstand internal carbonation pressure without dome distortion.
Precision control over crystal lattice structure and earing behavior during ironing ensures uniform wall thickness down to 0.081 mm at the middle body, while maintaining 0.265 mm at the bottom dome for burst pressure compliance (>6.2 bar / 90 psi).
To eliminate metal-beverage interaction and preserve organoleptic purity, internal coatings use next-generation BPA-Non-Intent (BPA-NI) acrylic or cross-linked modified polyester resins. Applied via high-pressure centrifugal spray nozzles, coatings are cured at precise thermal curves (200°C–210°C) to form a pinhole-free barrier.
The versatility of the global 330ml aluminum container platform extends across highly diverse product categories, each demanding customized neck profile specifications, internal lacquer weights, and top end closures (SOT, RPT, non-magnetic, or sterilisable formats).
Paired with 202# SOT (Stay-On Tab) ends. Designed to handle internal pressures up to 4.5 volumes of CO2. Pasteurisation-ready epoxy coatings withstand thermal shocks during tunnel pasteurization (60°C–65°C) without blistering.
Requires high-film-weight BPA-NI linings. Ethanol concentrations up to 15% ABV and high organic acid content demand superior chemical resistance to prevent aluminum ion leaching into premium cocktail formulations.
Utilizes liquid nitrogen dosing technology during filling. Nitrogen expansion pressurizes non-carbonated cans to build structural column strength for stacking, while providing a smooth creaming effect upon opening.
Formulated to resist low-pH matrix containing taurine, caffeine, citric acid, and mineral salts. High-precision necking ensures double-seam integrity under elevated filling speeds (>1,200 cans/minute).
Employs non-magnetic aluminum easy-open ends and odor-proof 206#/401# lids. Hermetically sealed under inert gas flush (N2/CO2) to achieve residual oxygen levels <0.5% for sensitive nutritional powders.
Paired with high-temperature sterilisable aluminum lids capable of withstanding steam autoclave cycles at 121°C for 45 minutes, assuring commercial sterility without seal degradation.
Navigating multi-regional regulatory frameworks requires strict compliance documentation and precise batch traceability. Our 330ml aluminum cans and closures comply fully with global food-contact standards, ensuring seamless importation and retail authorization across North America, the European Union, the Asia-Pacific region, and the Middle East.
Every batch of raw material and finished packaging is released with comprehensive certification proving compliance with major international food contact guidelines:
Double-seam integrity is paramount to leak prevention. Our technical team works alongside filling line engineers to optimize double-seam dimensions:
The evolution of the 330ml aluminum beverage container continues at a rapid pace. As global manufacturers strive for lighter footprint and enhanced consumer engagement, our R&D roadmap focuses on three core pillars of innovation over the coming decade.
Developing advanced alloy grain structures that permit reducing can sidewall gauge from 0.081 mm to 0.074 mm without losing axial column strength. This down-gauging initiative targets a 6% overall reduction in aluminum raw material consumption per 1,000 cans.
Transitioning internal and external protective coatings from solvent-based systems to 100% waterborne, plant-derived monomer resins. This transition reduces volatile organic compound (VOC) emissions during manufacturing to near zero while improving coating elasticity.
Integrating high-definition direct-to-shape digital printing with variable QR codes and embedded Near Field Communication (NFC) tabs. This allows brands to run dynamic marketing campaigns and provide anti-counterfeiting verification directly on individual 330ml cans.
Comprehensive answers to common engineering, logistical, and compliance questions faced by B2B buyers and beverage plant managers.
Discover our secondary suite of high-performance aluminum coils, specialty powder ends, sleek cans, and high-temperature sterilizable lids engineered for industrial packaging applications.