Explore our certified food-grade packaging components engineered for ultra-high speed filling lines and severe pressure environments.








Understanding the transition from traditional beer holders and carriers to high-integrity 2-piece drawn and ironed (DWI) aluminum beverage cans and SOT ends.
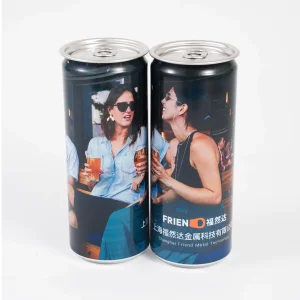
In the modern international beverage industry, the query for a High-Quality Beer Holder Manufacturer Service & Products spans across multiple critical operational layers. While historically "beer holder" referenced secondary packaging, plastic handles, or insulated sleeves, global enterprise buyers, brewmasters, and supply chain directors now define a beer holder as the entire primary containment and barrier delivery system. This encompasses 2-piece drawn-and-ironed (DWI) aluminum cans, Stay-On Tab (SOT) easy-open ends, rigid multi-pack carriers, and barrier-coated tinplate containers designed to lock in dissolved oxygen (DO) limits, withstand severe thermal pasteurization cycles, and maintain pressure resistance up to 6.2 bar.
To achieve sustainable operational margins, global beverage brands require manufacturing partners who combine raw material metallurgy (such as alloy temper optimization across 3104-H19 and 5182-H48 stocks) with intelligent factory automated inspection systems. As consumers rapidly shift away from single-use plastics and fragile glass bottles toward infinitely recyclable aluminum formats, the pressure on contract manufacturers and OEM/ODM packaging partners to deliver zero-defect double-seam compatibility has never been higher.
Technical Insight: Double-seam integrity is governed by precise dimensional parameters: Hook Length, Overlap, Countersink Depth, and Seam Thickness. A variation as small as 0.012mm in end-curl radius can lead to catastrophic micro-leakage during tunnel pasteurization at 65°C.
Deploying specialized alloys, surface passivations, and interior barrier coats across distinct liquid formulations and distribution conditions.
Craft beers contain volatile hop aromatics and living yeast cultures that require ultra-strict dissolved oxygen control and light barrier protection.
Mass-market brewing operations require high-speed filling line stability (exceeding 1,200 cans/minute) and extreme axial column strength.
High-acid formulas, spirits bases, and fruit juices present severe internal corrosion risks that require specialized protective barriers.
Comprehensive specifications for corporate procurement directors, quality assurance managers, and contract packaging engineers.
Selecting the correct metal specification requires aligning chemical composition, mechanical strain tolerances, and dimensional standards. Below is the technical procurement matrix maintained by our advanced engineering facility in Shanghai.
| Component Category | Alloy & Temper | Thickness Standard | Internal Liner System | Primary Application |
|---|---|---|---|---|
| Can Body (Standard/Sleek) | 3104-H19 Aluminum | 0.245mm – 0.275mm | Water-based Acrylic / BPA-NI | Beer, Cider, Soft Drinks, Sparkling Water |
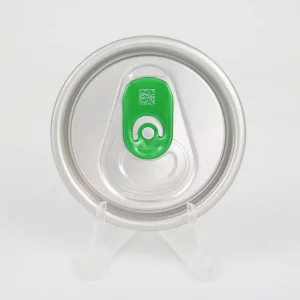
| Easy-Open End (SOT) | 5182-H48 Aluminum | 0.205mm – 0.225mm | Organosol / Non-BPA Vinyl | Pressurized Carbonated Drinks, Beer Cans |
| Pull Tab Mechanism | 5052-H38 Aluminum | 0.350mm – 0.380mm | Clear / Anodized Color Varnish | High-Leverage Tab Opening Systems |
| Powder & Dry Goods Lids | 8011-O / 3003 Aluminum | 0.180mm – 0.210mm | Food-Grade Heat-Seal Lacquer | Infant Formula, Coffee, Nutritional Powders |
| Preserve & Food Lids | MR Grade Tinplate (TH330) | 0.170mm – 0.230mm | Organosol / Aluminum Paste Epoxies | Retort Food Cans, Vegetables, Meat Products |
Enamel Rater & Porosity Testing: Every batch undergoes high-voltage enamel rating tests (NWA standard). Current conductivity readings are restricted to < 2.0 mA under 6.3V DC test conditions, guaranteeing that zero metal ions bleed into the beverage matrix to alter crisp malt flavor profiles.
How automated high-speed pressing, AI vision inspection, and digital supply integration eliminate defective units and ensure delivery timelines.
Utilizing multi-cavity high-precision presses from Stolle and Minister, capable of stamping out over 3,000 end shells per minute with tolerances within +/- 0.002mm.
High-resolution camera arrays inspect 100% of manufactured lids and can bodies in real-time, instantly rejecting units with scratch marks, compound voids, or tab misalignment.
Located near Shanghai Port, our automated warehouse facilities pack cans on customized wooden pallets with top frames, moisture barriers, and acoustic vibration damping.
Meeting rigorous international food contact standards while providing on-site technical assistance for seamer calibration.
Exporting food and beverage packaging across North America, the European Union, Asia-Pacific, and the Middle East requires flawless regulatory alignment. Every lot shipped from our facilities is accompanied by full chemical migration test documentation and batch traceability certificates.
Fully compliant with US FDA 21 CFR 175.300, EU Regulation 1935/2004, and China GB 4806.10 standards. Liners are verified free of BPA, heavy metals, phthalates, and fluorinated compounds (PFAS-free options available).
Our packaging engineers assist your filling plant team with seam teardown protocols, evaluating pin height, countersink depth, and hook overlap to eliminate operational downtime during product switching.
Leading the shift toward ultra-lightweight alloys, direct-to-shape digital decoration, and smart interactive packaging systems.
The global metal packaging landscape is undergoing a structural evolution driven by circular economy mandates and carbon footprint reductions. As a forward-thinking Beer Holder Manufacturer, our research and development initiatives focus on three key pillars:
Premium aluminum coil stock and specialty easy-open closures manufactured for global OEM clients.






Direct responses regarding minimum order quantities, seamer setups, pasteurization resistance, and custom artwork execution.
