Precision-engineered 500ml beverage cans, easy-open ends, and food-grade aluminum coil stock manufactured under strict ISO 9001 and FSSC 22000 standards.


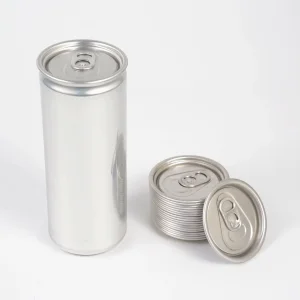




In-depth insights into why leading global beverage conglomerates are standardizing on the 500ml aluminum can format for craft beers, RTDs, energy drinks, and functional beverages.
The global beverage packaging industry has undergone a structural transformation over the past decade, driven by consumer demand for premium, infinitely recyclable, and shelf-stable packaging. At the forefront of this evolution is the 500ml aluminum can (often referred to as the European Pint or Standard King format). As a leading manufacturer and exporter operating advanced production facilities in China, we specialize in high-velocity Drawn and Wall Ironed (DWI) aluminum container manufacturing engineered strictly around international performance standards.
A 500ml aluminum can is far more than a simple metal container; it is a highly calibrated thermodynamic pressure vessel. Achieving structural integrity while minimizing metal weight requires sophisticated metallurgical chemistry. The body of a premium 500ml can is manufactured from 3104-H19 manganese-magnesium aluminum alloy coil. This alloy composition provides an optimized balance of high tensile strength (yield strength exceeding 270 MPa) and exceptional formability required for multi-stage wall ironing operations.
| Parameter | Standard 500ml Can Specification | Engineering Significance | Quality Control Standard |
|---|---|---|---|
| Body Alloy / Temper | 3104-H19 Aluminum Alloy | High tensile strength, optimized drawability, low earing behavior (<1.2%) | EN 485 / ASTM B209 Compliance |
| Lid Shell Alloy / Temper | 5182-H48 / 5182-H19 Alloy | High magnesium content engineered for extreme buckle pressure resistance | ISO 9001 Batch Certification |
| Nominal Fill Volume | 500 ml ± 2.0 ml at 20°C | Precision volumetric capacity ensuring accurate automated fill heights | ISO 8124 Volumetric Inspection |
| Can Height & Neck Diameter | 168.0 mm Height / 202 Neck (52.5mm) | 202 lightweight neck design reduces lid material while maintaining fill rate | Calibrated Laser Optical Gauge |
| Mid-Wall Thickness | 0.092 mm – 0.098 mm | Ultra-lightweighting gauge achieved via multi-stage wall ironing dies | Ultrasonic Wall Thickness Meter |
| Internal Buckle Strength | > 6.2 bar (> 90 PSI) | Prevents deformation under carbonation pressure and high-temp pasteurization | Pneumatic Destruction Testing |
| Axial Load Resistance | > 1.4 kN (> 140 kgf) | Ensures stacking stability during warehousing and international transit | Compression Testing Rig |
Our production facilities utilize tension-leveled 3104-H19 coils with strictly controlled planar anisotropy. By maintaining an earing ratio below 1.2%, our drawing and wall ironing processes eliminate uneven flange heights. This micro-level metallurgical control directly prevents double-seam micro-leaks and reduces trim scrap by 3.5%, delivering direct cost benefits to our enterprise buyers.
Combining vast raw material integration, state-of-the-art European high-speed press lines, and direct maritime logisitics out of Shanghai Port.
Our manufacturing hubs are strategically aligned with upstream aluminum smelting and rolling giants (Chinalco, Southwest Aluminum). This raw material proximity secures consistent 3104 and 5182 coil allocations even during global aluminum market squeezes.
We operate fully automated, ultra-high-speed cupping, ironing, and necking lines imported from industry pioneers like Minister, Belvac, and Stolle. Lines operate at speeds up to 3,000 cans per minute with 100% online optical camera inspection.
Whether you require short-run seasonal promotional craft beer cans or multi-million annual contracts for multinational beverage brands, our manufacturing footprint accommodates quick printing plate changes and flexible volume scaling.
Stay ahead of regulatory shifts, environmental legislation, and technological breakthroughs transforming the global beverage industry.
Global regulatory bodies (FDA, EFSA, France ANSES, China GB) are enforcing stringent phase-outs of Bisphenol A (BPA) and related phthalate plasticizers in food-contact materials. Our factory leads the transition with advanced BPA-NI (Bisphenol A Non-Intent) Acrylic and Polyester-based internal lacquers.
These next-gen internal coatings are cross-linked at precise oven bake temperatures (200°C–215°C) to create an impermeable chemical barrier. This prevents flavor scalping and guarantees zero chemical migration even when filled with aggressive, low-pH beverages (such as sour beers, carbonated mixers, kombucha, and cider with pH < 2.6).
With aluminum prices tied to energy indexes and corporate ESG targets mandating Scope 3 emissions reductions, lightweighting without sacrificing structural integrity is the ultimate engineering goal. Through finite element analysis (FEA) and computer-optimized necking dies, we have trimmed 500ml can body weights by over 8% compared to legacy specifications.
Every 1,000,000 lightweighted 500ml cans saves over 1.2 metric tons of primary aluminum ingot, directly reducing maritime ocean shipping costs and lowering carbon footprints for global brand owners.
Modern consumers buy with their eyes. Our 8-color high-speed dry-offset decorating presses achieve ultra-crisp photographic resolution (up to 133 LPI dot density) directly onto the aluminum container wall. Beyond standard color reproduction, we offer specialty sensory finishes:
Smart packaging is rapidly expanding into metal containers. We offer laser-etched matrix codes on the underside of 202 SOT / RPT easy-open tabs and high-speed inkjet coding on bottom domes. This allows beverage brands to run interactive consumer giveaways, track regional distribution logistics, and prevent grey-market diversion.
Optimized internal liner thickness, pressure thresholds, and end configurations customized to your specific beverage or food matrix.
The 500ml "Pint" format is the absolute gold standard for Craft IPAs, Stouts, Lagers, and Wheat Beers. Aluminum provides 100% barrier protection against UV light, completely eliminating the "skunking" phenomenon common in clear glass bottles.
Technical Setup: 202 SOT (Stay-On Tab) easy-open lid, internal epoxy or acrylic coating calibrated for dissolved oxygen (DO < 10 ppb target), pasteurization withstand capacity up to 60 PU at 62°C.
High-alcohol or spirit-based RTD (Ready-To-Drink) beverages present aggressive organic acid matrixes that can degrade standard internal coatings if improperly formulated.
Technical Setup: Modified high-build BPA-NI polyester lining (60-90 mg/sq.m coat weight), double-pass internal spray application, 202 RPT (Resealable Pull-Tab) or SOT lid options engineered for CO2 retention up to 4.2 volumes.
High-caffeine, taurine, and B-vitamin enriched functional formulations require robust container pressure stability for fast-moving automated grab-and-go retail shelves.
Technical Setup: High axial load resistance (>1.5 kN), custom colored aluminum tabs (black, red, blue anodized tabs) with laser-etched brand logos, high-speed filling line suitability (1,200+ cpm).
Non-carbonated beverages require internal liquid nitrogen (LN2) liquid dosing prior to seaming to create structural internal pressure (1.5-2.0 bar) for wall rigidity.
Technical Setup: Reinforced bottom dome radius to prevent dome inversion (bottom drop), specialized internal lacquers resistant to fatty acid oils present in dairy and oat milk additives.
Beyond liquid beverages, 500ml cans are widely adopted for luxury coffee beans, artisanal nuts, and specialty powders requiring hermetic moisture barriers.
Technical Setup: 200# or 300# full-aperture easy-open ends (FOE) with safety peel-off foil membranes, anti-static interior treatment, plastic over-caps for consumer resealability.
We bridge the gap between container manufacturing and your automated filling line through comprehensive seamer tooling integration and technical support.
The seam between the 500ml can body flange and the easy-open lid is the critical single point of failure in beverage packaging. A defective double seam leads to micro-leakage, beverage spoilage, and catastrophic shelf life loss. Our packaging engineers work directly with your plant technicians to calibrate your seaming rolls (Ferrum, Angelus, Continental, Krones, Hema).
We supply precise double-seam dimensional targets for every order batch:
Looking to stand out from standardized shelf profiles? We offer custom tool & die engineering for proprietary body shapes, embossed brand logos, textured wall fluting, and unique neck reduction angles (e.g., transitioning from 206 to 202 or 200 neck profile).
Our OEM/ODM Workflow guarantees seamless execution:
How we guarantee international regulatory compliance, zero-damage sea transport packaging, and risk-managed procurement for buyers worldwide.
Every shipment is issued with comprehensive food-grade compliance testing documentation verified by third-party laboratories (SGS, Intertek, TUV):
Empty aluminum cans are lightweight yet bulky, requiring engineered bulk palletization to maximize ocean container cube utilization while eliminating transit denting:
We work with enterprise purchasing teams to establish Total Cost of Ownership (TCO) efficiency contracts:
Direct technical answers from our Senior Packaging Engineers to address common procurement and production inquiries.
Explore our full line of non-magnetic, anti-static, and precision easy-open ends for beverage, pharmaceutical, and powder applications.







