High-performance metal packaging components designed to exceed stringent global hermetic seal, oxygen barrier, and structural integrity requirements.

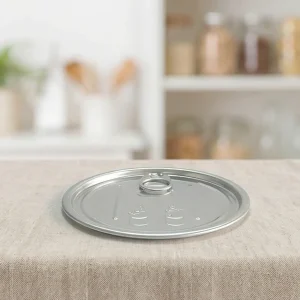






In the era of accelerating ESG (Environmental, Social, and Governance) mandates and regulatory shifts toward circular supply chains, aluminum packaging—spanning ultra-thin converter foil, container foil, cold-form blister foil, and rigid beverage cans—has emerged as the gold standard for sustainable enterprise packaging. As a leading manufacturer based in China's industrial manufacturing powerhouse, our operations integrate advanced metallurgical casting, high-precision foil rolling, eco-friendly lacquer chemistry, and automated end-converting technologies.
Global enterprise buyers in North America, Western Europe, the Middle East, and APAC face compound sourcing challenges: volatility in LME (London Metal Exchange) ingot prices, shifting Carbon Border Adjustment Mechanisms (CBAM), and high automated filling line speed requirements (often exceeding 1,200 to 1,500 cans per minute). Sourcing directly from top-tier Chinese manufacturers provides robust structural advantages, including complete vertical integration from aluminum ingot cast-rolling down to lacquered foil coil slitting and press stamping.
Achieving superior burst strength, drawability, and shelf-life stability requires precise alloy selection and specialized internal lacquer systems tailored to the chemical aggressiveness of the payload.
| Alloy Series | Temper State | Tensile Strength (MPa) | Elongation (%) | Primary Industrial Application |
|---|---|---|---|---|
| 8011 Aluminum | O / H18 / H22 | 125 – 165 | ≥ 3.0 % | Lidding foil, pharmaceutical blisters, milk powder barrier lids, household foil. |
| 3104 Aluminum | H19 | 275 – 310 | ≥ 4.0 % | Deep-drawn two-piece beverage can bodies (DWI process), high-strength containers. |
| 5182 Aluminum | H48 / H19 | 360 – 410 | ≥ 5.0 % | Easy-open end (EOE) shells, SOT (Stay-On Tab) lids requiring elevated buckle pressure. |
| 5052 Aluminum | H32 / H34 | 215 – 265 | ≥ 7.0 % | Pull-tab stock, rust-proof closure rings, anti-corrosive marine container caps. |
In response to US FDA 21 CFR 175.300 and EU Regulation (EC) No 1935/2004 compliance frameworks, our factory leads the industry in Non-Intent Bisphenol A (BPA-NI) coating technologies. We apply next-generation Acrylic, Polyester, and Organosol lacquers with precision roll-coaters, followed by high-temperature thermal curing ovens to guarantee:
Pin-hole free barrier coverage verified through high-voltage enamel rating tests (< 2.0 mA under standard 1% NaCl electrolysis).
Capable of surviving steam sterilization up to 121°C (250°F) for 30–60 minutes without coating blushing, feathering, or adhesion loss.
Formulated to resist aggressive organic acids, carbon dioxide expansion (up to 6.2 bar internal pressure), and essential oil breakdown.
Sourcing metal packaging components requires balancing technical seamer tolerance matching with global shipping density. Below is an engineering comparison matrix designed for procurement directors and packaging development engineers evaluating global suppliers:
Down-gauging foil and shell stock (e.g., reducing end gauge from 0.224mm to 0.208mm) cuts raw material costs by up to 6.8% while maintaining structural buckle pressure standards via optimized countersink geometry.
Full geometric mapping for high-speed Angelus, Ferrum, and CFT seamers. Custom curl diameter, countersink depth, and compound lining weight adjustments prevent seam cut-overs and false seam defects.
Optimized bulk palletization using corrugated top frames, anti-static plastic slip-sheets, and heat-sealed VCI moisture barrier shrink hooding ensures 100% rust-free ocean transit across tropical zones.
Complete batch-level traceability linking every shipped pallet directly to original aluminum coil mill certificates (MTC), lacquer heat codes, and hourly QC teardown logs.
To eliminate micro-defects in mass production, our conversion facilities integrate high-resolution optical camera vision systems, inline laser gauging, and automated pneumatic leak testing across every conversion press line.
Multi-angle camera arrays inspect 100% of easy-open ends for tab alignment, score-line micro-cracks, seal compound voids, and varnish scratches at speeds up to 3,000 pieces/minute.
Automated score-depth tooling adjusts dynamically based on continuous residual metal measurement, guaranteeing smooth pop-and-pull opening forces without risk of premature burst during pasteurization.
Destructive testing samples are subjected to step-up hydrostatic pressure up to 6.8 bar to verify end panel structural resistance against carbonation spikes.
Specialized lid engineering, transparent-top features, and sleek beverage container profiles tailored to consumer shelf-appeal and process safety.






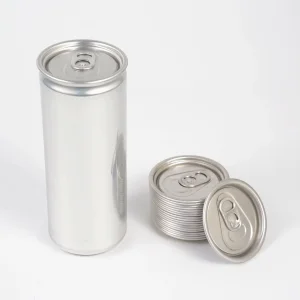

Navigating cross-border customs regulations, food-grade compliance, and logistics risks requires robust manufacturer backing. Our dedicated export engineering division provides end-to-end technical documentation and field service support across major international trade blocs.
Fully compliant with FDA 21 CFR 175.300 resin specifications and heavy metal threshold requirements (CONEG / Toxics in Packaging legislation).
Certified compliance with Regulation (EC) No 1935/2004, EU No 10/2011 migration testing, and SVHC (Substances of Very High Concern) absence guarantees under REACH.
100% synthetic, animal-fat-free lubricants and washing chemical systems ensuring complete compatibility with global Halal and Kosher food production guidelines.
Our packaging field engineers provide remote or on-site double-seam teardown calibration, optical seam profile inspection, and chuck/roll re-tooling advice.
In-depth technical answers addressing common engineering, sourcing, and quality assurance queries from prospective B2B clients.
