High-performance aluminum cans, easy-open ends, and specialty closures manufactured under rigorous ISO 9001 and FSSC 22000 quality standards.
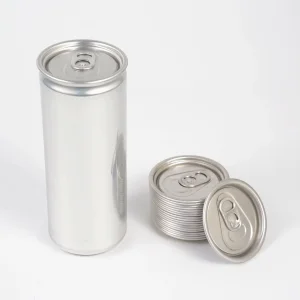






In the modern high-speed beverage packaging landscape, the 330ml Standard Aluminum Can represents the optimal convergence of metallurgical science, structural ergonomics, and sustainable circular logistics. As a leading manufacturer based in China, our operations integrate advanced deep-drawing technology, precision necking, and state-of-the-art chemical barrier application to fulfill the rigorous demands of global beverage brand owners, contract co-packers, and high-volume distributors.
The global transition from rigid glass and single-use PET toward infinitely recyclable aluminum is driven by strict decarbonization targets, Extended Producer Responsibility (EPR) regulations, and the European Carbon Border Adjustment Mechanism (CBAM). Aluminum beverage packaging retains over 75% of all metal ever refined in active economic circulation today. Re-smelting post-consumer aluminum cans requires only 5% of the energy compared to primary bauxite extraction, delivering up to a 95% reduction in Scope 1 and Scope 3 greenhouse gas emissions.
Closed-loop recycling allows a used 330ml aluminum body to be processed, re-melted, re-rolled, stamped, filled, and returned to retail shelves within 60 days.
Engineered for high-speed filling lines running at speeds up to 120,000 CPH (cans per hour) with zero downtime and minimal seamer jam rates.
Next-generation waterborne acrylic and modified polyester internal lacquers guarantee flavor neutrality and zero chemical migration into sensitive liquids.
Our standard 330ml format serves a wide spectrum of beverage categories including Carbonated Soft Drinks (CSD), Craft Beer, Hard Seltzers, Ready-to-Drink (RTD) Alcoholic Cocktails, Kombucha, Cold Brew Coffee, Sparkling Mineral Water, and Functional Energy Formulations. Each beverage profile demands specialized internal coating weight specifications and top-end pressure tolerances.
A granular breakdown of alloy chemistry, wall-thinning parameters, dome resistance dynamics, and precision necking technology.
| Technical Parameter | Standard 330ml Specification | Tolerance Standard | Testing & QA Protocol |
|---|---|---|---|
| Nominal Fill Volume | 330 mL | ± 2.0 mL | Volumetric Laser Displacement |
| Brimful Volume | 350 mL ± 3 mL | ISO 9001 Batch Inspection | Gravimetric Water Fill Test |
| Can Body Alloy | AA 3104-H19 (Mn-Mg Aluminum) | ASTM B209M Standard | Optical Emission Spectrometry |
| End Shell / Tab Alloy | AA 5182-H48 / AA 5052-H19 | Strict Temper Tolerance | Tensile Yield Strength Testing |
| Can Height | 115.20 mm | ± 0.30 mm | Digital Contact Micrometer |
| Can Body Diameter | 66.25 mm | ± 0.20 mm | Vernier Caliper / Go-NoGo Gauge |
| Neck Finish Code | 202 Diameter (52.5 mm fitment) | Standard Seamer Compatibility | Flange Profile Optical Scanner |
| Internal Pressure Rating | ≥ 6.2 bar (90 PSI) | Bottom Dome Deformation Limit | Pneumatic Hydrostatic Burst Tester |
| Axial Load Resistance | ≥ 1,000 N (225 lbf) | Compressive Strength Limit | Top-Load Compression Press |
| Enamel Conductivity | < 2.0 mA (Target < 1.0 mA) | Zero Pinhole Threshold | 1% NaCl Electrolytic Enamel Rater |
The manufacturing of our standard 330ml aluminum cans utilizes the Drawn and Wall Ironed (DWI) process. Coils of AA 3104-H19 aluminum are fed into high-speed cupping presses, where smooth circular shallow cups are formed. These cups pass through a series of tungsten carbide ironing rings that progressively reduce wall thickness while extending the height of the can body.
Advanced axial wall distribution enables us to engineer mid-body wall thicknesses down to 0.095 mm to 0.105 mm, while maintaining the thick top flange and bottom dome profile. This micro-gauge uniformity guarantees optimal strength-to-weight ratios, cutting shipping weight without sacrificing structural integrity under high stack loads.
Liquid products interact dynamically with metal substrates. To preserve flavor profiles and prevent organic acids (such as phosphoric, citric, or lactic acid) or dissolved carbon dioxide from attacking the metal, we apply state-of-the-art internal spray linings:
Automated high-speed production lines, AI-driven optical inspection, and direct Shanghai port logistics integration guarantee uninterrupted product flow.
Integrated equipment setups from industry leaders (Stolle, Belvac, Ragsdale) achieve operating speeds up to 3,000 cans per minute per line with sub-micron tolerance control.
100% inline high-definition camera arrays analyze every millimeter of the flange, neck, bottom dome, and internal spray coating, automatically ejecting defective units instantly.
Export pallets feature anti-humidity kraft slip sheets, heavy-duty wooden top frames, automated high-tension stretch wrapping, and desiccant packs for ocean transport protection.
Operating from China's primary manufacturing hubs adjacent to Shanghai Port gives our clients a distinct cost and speed advantage. We maintain strategic long-term aluminum coil reserve agreements directly with tier-1 smelters, allowing us to offer flexible spot pricing, commodity hedging solutions, and stable lead times—even during global supply chain disruptions.
Ensuring seamless fitment with high-speed seamer equipment (Angelus, Ferrum, FMC, Cantronic) and total double seam mechanical security.
A double seam is the critical mechanical hermetic seal formed between the can body flange and the easy-open lid curl. Our technical team works directly with client engineers to establish optimal double seam dimensions:
Elevate brand presence on crowded retail shelves with advanced high-definition dry-offset metal printing technologies:
Pioneering sustainable breakthroughs, ultra-lightweighting gauge reductions, and intelligent digital packaging passes.
Advancing body coil down-gauging targets from 0.230mm to 0.210mm while maintaining full 6.2 bar internal pressure resistance through re-engineered dome geometry.
Transitioning coil procurement toward 100% hydro-powered smelter supplies, drastically dropping product-embedded carbon footprint for global ESG compliance.
Laser-etching unique high-speed QR and Data Matrix codes on individual lid tabs for farm-to-shelf traceability, engagement, and anti-counterfeiting.
Navigating global food contact regulatory frameworks requires rigorous documentation and constant testing. Every shipment of our 330ml standard aluminum cans and easy-open ends leaves our facility with a comprehensive batch testing certificate package.
Our commitment extends beyond delivering product to your loading dock. We provide specialized field engineering services to support your operational efficiency:
Explore our full selection of aluminum cans, specialty ends, tinplate closures, and premium coil stock.






Detailed engineering insights and commercial answers provided directly by our senior metal packaging specialists.
AA 3104-H19 is a specialized manganese-magnesium aluminum alloy formulated specifically for Drawn and Wall Ironed (DWI) packaging. The 'H19' temper indicates full strain-hardening, imparting maximum yield strength (≥ 270 MPa) and ultimate tensile strength (≥ 290 MPa). This high strength allows ultra-thin mid-body walls (0.095mm) capable of resisting high internal carbonation pressure without permanent deformation.
All our BPA-NI lining raw materials are sourced from globally certified coating providers (such as AkzoNobel and PPG). Each chemical batch undergoes Gas Chromatography-Mass Spectrometry (GC-MS) testing to confirm zero intentional addition of Bisphenol compounds. Every batch of cured cans is tested with a 1% NaCl electrolytic enamel rater, maintaining a conductivity threshold below 1.5 mA, ensuring complete pinhole-free barrier isolation.
Our standard 330ml can body paired with a 202# SOT (Stay-On Tab) 5182-H48 end is rated to withstand a minimum internal hydrostatic pressure of 6.2 bar (90 PSI) prior to bottom dome bucking. For pasteurized products like craft beer or high-carbonation soft drinks (up to 4.2 volumes of CO₂), this provides a minimum safety margin factor of 1.5x under warm tropical ambient logistics conditions.
For plain (unprinted/bright) 330ml cans, the standard MOQ is one 40ft High Cube container (approx. 150,000 to 180,000 units depending on pallet configuration). For custom 8-color offset printed cans, the production run MOQ is 300,000 units per design SKU to optimize print station setup, plate mounting, and ink ramp-up efficiency.
Finished cans are stacked on heat-treated solid wooden or plastic pallets, protected by top-and-bottom rigid layer cards, enclosed with moisture-impermeable polyethylene stretch-hood film, and secured with vertical polymer strapping. Ocean containers are outfitted with high-capacity desiccant bags to absorb ambient humidity fluctuations across tropical routes.
