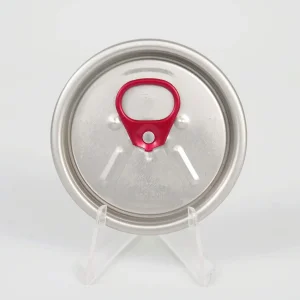
Engineered for high-speed filling lines, superior hermetic sealing, and international food-contact compliance.





The global rigid metal packaging market is undergoing a seismic technological shift driven by three primary catalysts: strict decarbonization mandates, evolving food safety regulations regarding end-line migration, and the explosive growth of single-serve canned beverages and specialized nutritional powders. As global brand owners pivot away from single-use plastics to meet carbon neutrality targets, the demand for high-performance Easy Open Ends (EOE)—encompassing Stay-On Tab (SOT), Ring Pull Tab (RPT), and specialized full-aperture peel-off foils—has reached unprecedented levels.
Modern high-speed beverage filling lines operating at speeds up to 2,000 Cans Per Minute (CPM) require absolute dimensional consistency in lid curl diameter, score depth uniformity, and compound weight placement. A variation of merely ±0.005mm in countersink depth or shell thickness can cause micro-leaks, seamer jams, or catastrophic buckle failures during thermal pasteurization or pressure loading. China's global metal packaging manufacturing ecosystem has emerged as the premier global supplier of easy-open ends, leveraging fully automated, high-speed stamping presses from world-class machine builders (such as Stolle, Minster, and Schuler) integrated with domestic high-purity aluminum alloy coil production.
Engineered using premium 5182-H48 and 3104-H19 aluminum alloys. Lightened shell profiles reduce material consumption by up to 8% while maintaining internal buckle resistance exceeding 6.2 bar (90 PSI).
Complete compliance with global regulatory mandates (FDA 21 CFR 175.300, EU 1935/2004, GB 4806.10). Advanced organosol and acrylic BPA-NI (Non-Intent) linings eliminate flavor scalping and heavy metal leaching.
Optimized curl height, feathering control, and precise lining compound distribution allow seamless seamer integration across Ferrum, Angelus, and FMC high-speed seaming stations without machine stopping.
Comprehensive standard parameters for global beverage fillers, dry powder packaging plants, and food canneries.
Selecting the correct Easy Open Lid size and material specification is critical to maintaining thermal vacuum integrity, preventing gas loss in carbonated beverages, and eliminating moisture intrusion in hygroscopic dry powders (such as infant formula and pharmaceutical powders). Below is the comprehensive technical matrix across primary standard industry lid diameters:
| Industry Code | Nominal Diameter | Primary Alloy / Temper | Tab & Design Type | Buckle Resistance | Pop / Pull Force | Target Applications |
|---|---|---|---|---|---|---|
| 200# | Ø 50mm | Aluminium 5182-H48 | SOT / Sleek & Slim Profile | ≥ 6.2 bar (90 PSI) | Pop < 22N / Pull < 32N | Energy drinks, craft beer, sleek carbonated water |
| 202# SOT | Ø 52.5mm | Aluminium 5182-H48 / 5052 Tab | Stay-On Tab (SOT) Standard | ≥ 6.5 bar (94 PSI) | Pop < 24N / Pull < 35N | Standard CSD, RTD coffees, hard seltzers, lager beer |
| 202# RPT | Ø 52.5mm | Aluminium 5182-H48 | Ring Pull Tab / Resealable Option | ≥ 6.0 bar (87 PSI) | Pop < 20N / Pull < 30N | Juices, non-carbonated functional drinks, RTD teas |
| 206# | Ø 56.4mm | Aluminium 5182 / 3104 Lacquered | Full Aperture / Odor-Proof Barrier | ≥ 2.5 bar (Vacuum) | Pop < 18N / Pull < 28N | Gourmet coffee beans, spices, milk powders, nuts |
| 209# | Ø 62.5mm | Aluminium 5182-H48 | Full Aperture Easy Open (FA EOE) | ≥ 2.0 bar (Vacuum) | Pop < 25N / Pull < 38N | Pet food, canned fruits, snack cans, dry herbs |
| 300# | Ø 73mm | Food-Grade Tinplate / ETP / TFS | Ring Pull Full Aperture | Retort Proof (121°C) | Pop < 28N / Pull < 42N | Canned meat, fish, ready-to-eat meals, soups |
| 307# | Ø 83.3mm | Tinplate / Aluminum Alloy | Full Aperture / Peel-Off Foil | Retort Proof (121°C) | Pop < 30N / Pull < 45N | Vegetables, tomato paste, pet foods, milk powder |
| 401# | Ø 99mm | Electrolytic Tinplate / Aluminum | Full Aperture / Safety Rim | Nitrogen Flush Compatible | Pop < 32N / Pull < 48N | Infant formula, protein powders, coffee tins, nuts |
| 502# | Ø 127mm | Aluminium / Tinplate Composite | Peel-Off Foil / Transparent Lid | Airtight Hermetic Vacuum | Easy-Peel Force < 15N | Bulk infant formula, commercial powders, pet food |
End-to-end supply chain integration, advanced metallurgy, scale economics, and rigorous QA protocol.
China controls the complete upstream-to-downstream aluminum lifecycle—from high-purity smelting and precision alloy hot-rolling (3104/5182/8011 coils) to high-speed conversion press lines. This guarantees raw material price stability and continuous production cycles during global supply panics.
Leading Chinese factories utilize ultra-precision carbide dies and online Vision Inspection Systems capable of scanning 100% of manufactured lids for micro-pinholes, score line cracks, tab alignment faults, and edge burrs at speed thresholds exceeding 1,500 parts per minute.
Equipped with state-of-the-art CTP pre-press tooling, Chinese manufacturers offer laser-etched QR codes on tab undersides for promotional campaigns, custom color anodized tabs, embossed brand logos, and multi-color rim printing with low minimum order quantities (MOQ).
Customized chemical lacquer systems, internal pressure designs, and barrier technologies tailored for diverse market sectors.
Packaging integrity is highly product-dependent. A lid formulated for non-carbonated tea will fail catastrophically if applied to a high-pressure craft beer or an acidic carbonated beverage. Chinese EOE manufacturers provide specialized macro-solutions engineered for specific product matrices:
Primary Model: 202# SOT & 200# SOT Aluminum Lids
Requires high internal pressure resistance (up to 6.5 bar) to withstand carbonation expansion and hot water pasteurization tunnels (60–65°C for 20 minutes). Coated with organosol lacquers to resist alcohol attenuation and carbonic acid degradation.
Primary Model: 401# & 502# Peel-Off Foil / Easy Open Lids
Demands total zero-oxygen permeability, low nitrogen gas loss during MAP (Modified Atmosphere Packaging), and smooth anti-scratch safety rims. Manufactured in ISO Class 8 cleanrooms to prevent particulate contamination.
Primary Model: 300#, 307#, 401# Tinplate / Aluminum FA EOE
Designed to undergo harsh thermal retort sterilization (121°C to 131°C under pressure for 30–60 minutes). Features double-coated gold/organosol linings that prevent sulfur staining, iron dissolution, and seal delamination.
Step-by-step verification checklist to ensure smooth cross-border sourcing, seamer setup, and zero-defect delivery.
When auditing a Chinese Global Easy Open Lid manufacturer, global procurement teams must look beyond unit pricing. Ensuring long-term operational success requires auditing the factory’s raw material traceabilities, laboratory testing gear, and seamer setup support:
Expert answers to the most common engineering, procurement, and logistics inquiries from international buyers.
SOT (Stay-On Tab) ends are designed so that after opening, the tab and the score rivet remain permanently attached to the lid shell. This design is mandatory in most countries for carbonated beverage and beer cans to prevent littering and facilitate aluminum recycling. RPT (Ring Pull Tab) ends allow the tab and the score panel to detach completely from the can, which is preferred for non-carbonated liquids, juices, dry powders, or canned foods where an unobstructed pour or complete aperture access is required.
Leading Chinese manufacturers utilize raw coil pre-coated with certified BPA-NI lacquers supplied by premium global coating manufacturers (such as AkzoNobel, PPG, or Valspar). These internal coatings are formulated using polyester, modified acrylic, or polyorganosol resins that contain no bisphenol compounds. Every batch is validated via gas chromatography-mass spectrometry (GC-MS) testing and accompanied by SGS/Intertek migration certificates satisfying FDA 21 CFR 175.300 and EU Regulation 10/2011.
To seamlessly integrate a new lid supplier into your high-speed seaming equipment (e.g., Angelus, Ferrum, Pneumatic Scale), three parameters must match your current chuck setup: (1) Shell Curl Height & Radius: Determines how the lid feeds into the seaming turret; (2) Countersink Depth: Must align perfectly with your seaming chuck profile; and (3) Gasket/Lining Compound Weight: Ensures sufficient rubber compound flows into the double seam hooks during First and Second Operation seaming.
Easy Open Ends are packed under automated cleanroom conditions. Lids are stacked into heavy-duty paper or polyethylene sleeves (wraps), sealed tightly against moisture, and packed into corrugated fiberboard shipping cartons or wooden pallets with top frames. Desiccant packs are inserted into every box to absorb humidity during cross-equatorial ocean transit. Pallets are fully shrink-wrapped with stretch hood film and edge protectors to withstand high humidity and physical shock.
For standard unprinted aluminum beverage ends (e.g., 202# SOT or 200# SOT with standard clear internal lining), stocked inventory allows trial orders starting from 200,000 pieces with lead times of 10 to 15 days. For custom designs—such as laser-etched promotional codes, custom color tabs, rim logo printing, or specialized non-standard sizes—the MOQ typically ranges from 500,000 to 1,000,000 pieces per batch, with production lead times of 20 to 30 days following artwork approval.
Explore our complete catalog of food-grade tinplate lids, lacquered aluminum coils, and odor-proof closure solutions.