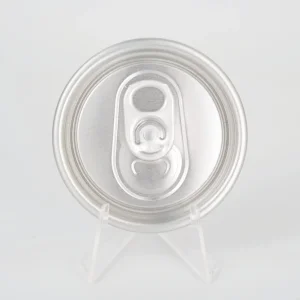
Direct factory supply solutions tested for double-seam integrity, micro-leakage prevention, and strict food-grade compliance.
An exhaustive analysis of demand dynamics, metallurgical innovations, and international packaging shifts.
The global metal packaging market is undergoing a seismic structural shift toward circular economic models and total hermetic safety. At the center of large-format rigid packaging lies the 509 Easy Open End (EOE)—also internationally recognized in metric sizing as the 127mm nominal diameter end (or 502/509 trade designator). Originally specified for high-capacity milk powder tins and industrial food services, modern 509 EOEs are now indispensable across specialized sectors including premium coffee bean storage, infant nutritional formulas, processed agricultural yields, and chemical formulations.
Global buyer demand for 509 Easy Open Ends is heavily concentrated in North America, Europe, the Middle East, and Latin America. However, regional manufacturing dynamics have compelled global buyers to pivot toward major production hubs in China. Production of the 509 diameter requires immense capital expenditure in high-tonnage multi-die stamping presses, laser-guided inspection systems, and advanced scoring depth calibration equipment. China's industrial ecosystem has consolidated this specialized capability, establishing over 500 dedicated, highly automated production centers capable of maintaining structural tolerances within a fraction of a micron.
Transition from Rigid Ends to Full-Aperture Pull-Tab Ends: Consumers globally demand total accessibility without requiring separate mechanical can openers. The 509 full-aperture aluminium and tinplate easy open end provides an immediate, safe, and clean peel/pull experience for large-diameter cans.
Strict Nitrogen-Flush & Oxygen-Barrier Requirements: Products like infant formula, roasted coffee beans, and clinical nutritional powders degrade rapidly when exposed to trace oxygen. Modern 509 EOE structures integrate advanced sealing compounds (such as high-solid water-based synthetic latex) that achieve hermetic sealing performance under vacuum pressures down to 0.02 bar.
How Chinese direct-manufacturing hubs deliver unparalleled cost efficiency, metallurgical stability, and production scalability for international B2B buyers.
Utilizing high-speed Minster and Stolle conversion presses operating at up to 1,200 ends per minute per lane. This scale drastically lowers unit production costs while eliminating mechanical variance across batch runs.
Raw materials sourced from tier-one aluminum rolling mills (5182-H48 shell stock, 5052 tab stock, and prime MR-grade tinplate). Application of advanced BPA-NI, Organosol, and Epoxy-Phenolic interior lacquers guarantees chemical resistance.
Integrated high-resolution camera detection systems automatically scan every single 509 lid for pinholes, score fractures, compound placement gaps, and surface scratches prior to automated high-density packaging.
| Technical Parameter | Aluminium Specification (509 EOE) | Tinplate Specification (509 EOE) | Quality Assurance Benchmark |
|---|---|---|---|
| Nominal Diameter | 127 mm (509 #) | 127 mm (509 #) | ±0.05 mm Tolerance |
| Substrate Alloy / Temper | Alloy 5182-H48 / Tab: 5052-H19 | MR Grade Tinplate, Temper T3/T4 | Mill Certificate Included |
| Base Material Gauge | 0.26 mm – 0.28 mm | 0.22 mm – 0.25 mm | Thickness Micro-Caliper Verified |
| Score Line Residual | 0.060 mm ± 0.005 mm | 0.055 mm ± 0.005 mm | Pop Force < 35N, Pull Force < 50N |
| Internal Lacquer Coating | BPA-NI / Organosol / Epoxy Phenolic | Gold / Clear Organosol / Modified Epoxy | Enamel Rater Test < 5mA |
| Sealing Compound Weight | Water-based Synthetic Rubber (400-600mg) | Water-based Synthetic Rubber (450-650mg) | Laser Optical Measurement |
| Buckle Resistance | > 2.2 bar | > 2.5 bar | Pneumatic Pressure Testing |
From sterile infant nutrition lines to high-humidity coastal warehousing, see how engineered 509 ends protect product integrity across distinct environments.
Requires absolute barrier perfection. The 509 EOE paired with a foil membrane rim ensures 0% moisture ingress, preventing clump formation and bacterial growth. Compatible with gassing systems achieving <0.5% residual oxygen.
Preserves volatile aromatic compounds and essential oils. Customized interior coatings resist acidity and oil migration while providing structural rigidity under varying ambient pressure during air transport.
Prevents rancidity caused by light exposure and ambient humidity. High-tensile pull tabs ensure smooth removal without sharp jagged edges, improving consumer safety and brand perception.
Strategic guidance for procurement directors, packaging engineers, and supply chain operators navigating regulatory compliance and sustainability.
1. Ultra-Lightweighting (Gauge Reduction): Through finite element analysis (FEA) and advanced ribbing designs, factories are reducing gauge thickness from 0.28mm down to 0.24mm without sacrificing buckle pressure resistance. This yields up to an 11% carbon reduction per million units shipped.
2. Transition to Non-Intent BPA Coatings (BPA-NI): Regulatory frameworks across the EU (EFSA updates) and North America (FDA requirements) are forcing a complete phase-out of traditional bisphenol-A epoxy liners. Chinese export-focused factories now lead in applying acrylic and polyester-based BPA-NI inner sprays that comply fully with EU Regulation 1935/2004 and FDA 21 CFR 175.300.
3. Smart Packaging Integration & Laser QR Scoring: High-end 509 easy open ends are increasingly customized with under-tab laser etched QR codes and anti-counterfeiting micro-prints for direct consumer marketing and product traceability.
Expert technical responses to common challenges encountered during seaming, logistics, and quality assurance.
Explore our full ecosystem of precision-engineered aluminum coil, tinplate ends, freeze-resistant lids, and specialized powder closures.