The 2026 global packaging market is placing greater pressure on manufacturers to deliver reliable, lightweight, and recyclable can solutions. Aluminum Can Packaging remains important for beverages, food products, personal care, and other regulated consumer categories. Its strength protects products during transport, while its recyclability supports more responsible resource use.
This guide examines leading aluminum can manufacturers worldwide through practical industry criteria. These include production capacity, forming technology, printing quality, coating performance, recycled content, quality control, and delivery consistency. It also considers regional reach, customer communication, customization capabilities, and documented sustainability practices. A strong manufacturer should provide more than attractive cans. It should offer stable dimensions, clean finishes, dependable seams, and clear technical support.
Details matter. A small printing mismatch can affect an entire retail launch. A weak coating may create problems after filling, stacking, or prolonged storage. However, no international ranking can reflect every buyer’s needs. Company information may change, and public sustainability claims require careful verification. That limitation deserves attention.
The manufacturers featured in this overview are therefore assessed with a balanced, evidence-aware approach. Certifications, factory capabilities, customer experience, and independent documentation should be reviewed before any purchasing decision. Some suppliers may excel in large-volume production, while others may offer better flexibility for regional brands or specialized designs. The best choice depends on product requirements, market location, budget, and compliance expectations. This 2026 overview aims to support informed comparisons, not replace professional supplier audits.
An industry-leading aluminum can packaging manufacturer combines production accuracy with practical customer experience. Modern plants use high-speed forming lines, automated vision inspection, and precise wall-thickness control. These systems reduce dents, leaks, and inconsistent printing. Still, automation is not enough. Skilled technicians must understand how small changes in metal temper affect filling-line performance. Reliable manufacturers also provide traceable material records, batch testing, and documented quality controls. That evidence matters more than attractive claims.
Sustainability is now measurable. Leading manufacturers increase recycled aluminum content, reduce process energy, and design lighter cans without weakening the body. They should share data from credible assessments, not vague environmental language. Food-contact safety, coating performance, and migration testing require strict technical discipline. Supply continuity matters too. Regional production capacity, realistic lead times, and emergency planning protect customers from costly interruptions. No factory is flawless. A trustworthy supplier admits limitations, investigates defects openly, and improves its process after failure.
Tips: Request sample cans and test them on your actual filling equipment. Check seam strength, coating resistance, print durability, and dimensional consistency. Ask for recent audit records and recycled-content verification. Compare total operating value, not only the unit price. A cheaper can may create slower lines, more waste, or hidden inspection costs. Also, review communication speed. Small delays can become expensive.
Modern aluminum can production combines high-speed forming with strict process control. The International Aluminium Institute reports that recycling aluminum can require up to 95% less energy than producing primary metal. This makes recycled-content management a major manufacturing concern.
Manufacturers begin with rolled aluminum sheet, commonly measured by thickness, temper, and coating performance. A cupping press forms flat blanks into shallow cups. Draw-and-iron machines then reduce wall thickness while extending the can body. Precision matters here. Small tool wear can create wrinkles, cracks, or uneven bases. Internal spray coating protects the metal from beverages, while external decoration uses high-speed digital or offset printing systems. Vision inspection checks dents, coating gaps, neck dimensions, and flange accuracy. The Can Manufacturers Institute identifies lightweighting and recycling efficiency as continuing priorities across the sector. Yet thinner walls can reduce tolerance for poor handling. That trade-off deserves honest testing.
Tips: Ask suppliers for line-speed records, gauge-control data, coating migration tests, and recycled-content verification. Review rejected-can rates, not only headline capacity. A factory may appear efficient while hiding unstable setup losses. Pilot trials with real filling conditions are safer than relying on laboratory samples. Temperature, pressure, and transport vibration can expose weaknesses. Good documentation helps, but it never replaces hands-on inspection.
| Production Stage | Key Manufacturing Technology | Common Materials or Components | Typical Industrial Parameters | Quality and Performance Objective | Sustainability Contribution |
|---|---|---|---|---|---|
| Material Selection | Alloy specification and coil sourcing | Aluminum alloy 3104 is widely used for can bodies; alloy 5182 is commonly used for easy-open ends | Coil temper, thickness, surface condition and mechanical properties are controlled before forming | Stable forming behavior, adequate strength and resistance to cracking during high-speed production | High recycled-content aluminum can be incorporated when alloy chemistry and quality requirements are maintained |
| Blanking and Cupping | High-speed stamping and deep-drawing of circular blanks | Lubricated aluminum sheet or coil | Circular blanks are formed into shallow cups with controlled draw depth and material flow | Uniform cup walls, minimized wrinkles and consistent metal distribution | High material utilization reduces trim waste compared with less efficient forming routes |
| Drawing and Ironing | Two-piece draw-and-wall-ironing, commonly abbreviated as D&I | Aluminum body stock formed into an integral can body and bottom | Several ironing rings reduce wall thickness while increasing can height; body-wall gauges are commonly below 0.15 mm in lightweight designs | Precise wall thickness, strong domed bottom and reliable pressure resistance | Lightweighting lowers aluminum consumption and transportation weight per filled container |
| Trimming and Body Shaping | Rotary trimming, profiling and controlled neck formation | Drawn aluminum can body | The open end is trimmed to a precise height; necking progressively reduces the diameter near the top | Accurate can height, smooth flange geometry and compatibility with the selected end diameter | Reduced neck and end diameters can lower metal use while preserving package performance |
| Washing and Surface Preparation | Multi-stage can washing, rinsing and drying | Water-based cleaning chemistry and treated process water | Removal of forming lubricant and aluminum fines before internal and external coating | Clean, chemically active surface with strong coating adhesion and controlled appearance | Closed-loop water treatment and optimized rinsing can reduce water consumption and wastewater load |
| Internal Protective Coating | Spray application of food-contact internal lacquer followed by thermal curing | Food-contact coating selected for beverage acidity, carbonation and storage conditions | Coating coverage, cure profile and defect level are monitored across the internal surface | Prevents metal-to-product interaction, corrosion, flavor impact and loss of package integrity | Low-solvent or water-based systems and efficient curing can reduce process emissions |
| External Coating and Printing | Roll coating, offset lithographic printing, varnishing and UV or thermal curing | Exterior basecoat, low-migration inks and protective over-varnish | Multi-color graphics are registered to the can profile; ink coverage and cure are inspected inline | Color consistency, scuff resistance, barcode readability and high-speed filling-line compatibility | Digital inspection and optimized ink laydown help reduce rejected decorated cans and material waste |
| Easy-Open End Production | End-shell stamping, scoring, riveting and tab assembly | Aluminum end stock, scored opening panel, riveted pull tab and sealing compound | Score depth, rivet dimensions, tab placement and compound application are tightly controlled | Reliable opening force, tamper evidence, leak prevention and safe consumer handling | Lightweight end designs reduce metal use; aluminum components remain suitable for recycling |
| Flanging and Seaming | Can flanging followed by double seaming during filling and closing | Prepared can body, easy-open end and sealing compound | First- and second-operation seam rolls form a hermetic double seam; seam measurements are verified by inspection | Hermetic seal, resistance to pressure and protection against leakage or contamination | Reliable seaming reduces product loss, recalls and packaging waste throughout distribution |
| Inline Inspection | Machine vision, sensor-based dimensional checks and leak testing | Finished can bodies, decorated cans and assembled ends | Typical checks include pinholes, dents, coating defects, flange geometry, print registration and seam integrity | Early detection of defects, traceable process control and consistent package safety | Automated defect removal prevents large batches of nonconforming packaging from entering the supply chain |
| Process Automation | PLC-controlled lines, robotics, predictive maintenance and manufacturing data systems | Forming presses, washers, decorators, inspection units and palletizing equipment | Real-time monitoring of speed, temperature, pressure, lubricant flow, coating weight and downtime | Higher equipment availability, repeatable quality and faster root-cause analysis | Energy monitoring and optimized operating conditions can reduce electricity, compressed air and lubricant use |
| Recycling and Scrap Recovery | Segregation, baling, remelting and alloy management | Post-industrial aluminum scrap, used beverage cans and production trim | Scrap is sorted and remelted into controlled alloy streams for new sheet or other aluminum products | Material recovery, controlled chemistry and reduced dependence on primary aluminum | Recycling aluminum generally requires substantially less energy than producing primary aluminum from ore |
| Compliance and Documentation | Food-contact compliance, batch traceability and quality-management systems | Materials, coatings, inks, compounds and finished packaging | Testing and documentation commonly address migration, coating adhesion, seam integrity and dimensional conformity | Regulatory conformity, product safety and consistent customer qualification | Documented process control supports responsible sourcing, waste reduction and lifecycle reporting |
Note: Parameters shown are representative industry practices and may vary according to can format, beverage type, equipment configuration, regional regulations and customer specifications.
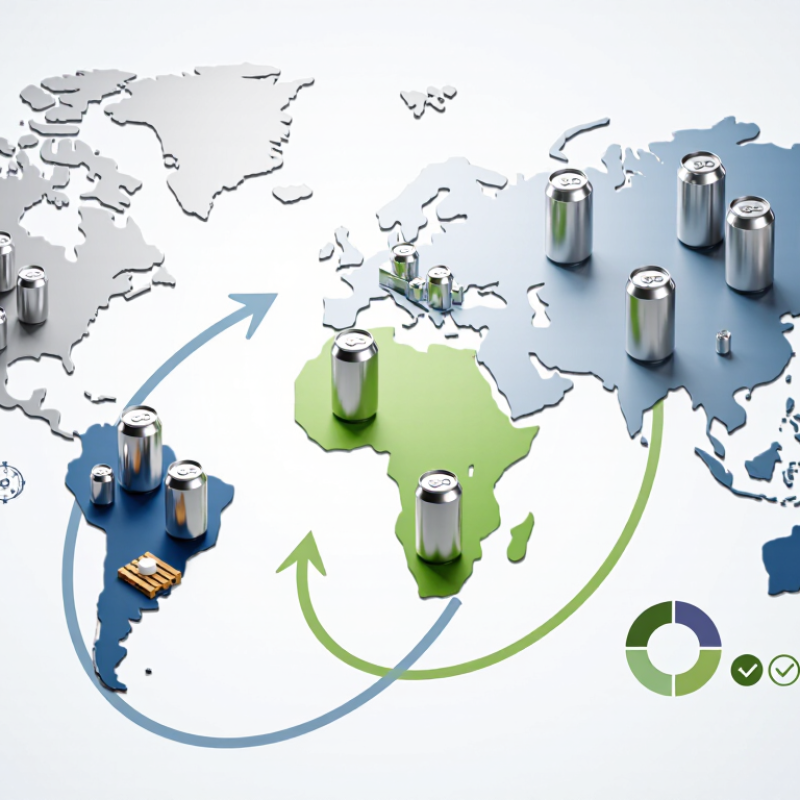
Aluminum can packaging demand is expanding across beverage, food, and personal care markets. Regional needs differ sharply. North America values lightweight formats, recycled content, and dependable high-volume supply. Europe places stronger emphasis on circular systems, collection rates, and documented carbon performance. Regulations matter every day.
Asia-Pacific remains the largest growth area, supported by urban populations and rising convenience consumption. China, India, Japan, and Southeast Asia require different can sizes, printing standards, and delivery models.
Latin America shows strong potential, especially where modern retail and local beverage production are developing. The Middle East and Africa need suppliers that can manage heat, transport distance, and uneven recycling infrastructure.
Tips: Compare more than unit price. Ask manufacturers about recycled aluminum percentages, wall-thickness control, food-contact testing, and batch traceability. Review sample cans under real filling and storage conditions. A can that looks perfect may still fail during high-speed production. Regional warehouses can also reduce delays, but they may increase inventory costs.
In 2026, reliable manufacturers should demonstrate process consistency, technical support, and transparent environmental data. Certifications help, but site audits reveal more. Buyers should check press quality, seam integrity, coating performance, and complaint response times. Forecasts can miss sudden shifts in energy prices or consumer preferences. That uncertainty deserves a practical backup plan.
Sustainability now depends on measurable factory practices, not attractive claims. Leading aluminum can manufacturers should document recycled content, energy use, water consumption, and material losses. The International Aluminium Institute reports that recycling aluminum requires about 5% of the energy used for primary production. That difference makes closed-loop can recycling commercially important. It also makes collection quality essential.
Manufacturers should align operations with ISO 14001 environmental management requirements and use credible chain-of-custody systems. The Aluminium Stewardship Initiative’s standards assess emissions, waste, labor conditions, and responsible sourcing across the value chain. In Europe, industry data reported beverage-can recycling at approximately 76% in 2023. However, regional performance varies sharply. The U.S. Environmental Protection Agency recorded a 45.2% recycling rate for aluminum beer and soft-drink cans in its 2018 national estimates. Older data still exposes a serious gap.
The can is rarely the weakest link.
Sorting facilities need compatible sensors, reliable baling, and stable access to remelting plants. Coatings and inks should support efficient processing without contaminating recovered metal. Manufacturers can also reduce transport emissions through lighter gauges, but excessive lightweighting may affect dent resistance and filling-line performance. That trade-off deserves testing, not optimism. Buyers should request third-party verified lifecycle data, factory audit results, and clear recycled-content calculations. A certificate alone proves little. The industry has strong technical potential, yet recycling systems remain uneven, and reported percentages may use different boundaries. Better disclosure would make comparisons fairer and purchasing decisions more reliable.
Choosing an aluminum can packaging manufacturer requires more than comparing unit prices. Audit its material source, production controls, testing records, and delivery performance. The International Aluminium Institute reports that recycled aluminum uses about 95% less energy than primary aluminum production. Therefore, request verified recycled-content data, scrap recovery rates, and evidence of closed-loop material handling.
Inspect the factory’s quality system, forming lines, coating controls, and dimensional testing. ISO 9001 certification helps, but it does not replace production records. Ask for batch traceability, defect rates, pressure-test results, and documented corrective actions. The Global Aluminum Can Stock Sustainability Report also highlights the importance of lightweighting and recycling infrastructure. A lighter can may reduce emissions, yet excessive material reduction can increase denting and transport losses.
Evaluate capacity with caution. A supplier may show impressive annual output, but available capacity during peak seasons matters more. Review lead times, minimum order quantities, tooling ownership, and contingency plans for metal shortages. Check whether the manufacturer can support different can sizes, printing requirements, and regional compliance documents. Numbers need context. Factory visits reveal details that spreadsheets miss, such as damaged pallets or inconsistent warehouse humidity. My own assessment would not rely on certification alone. It is useful, but imperfect. Ask again when answers sound too polished.
It combines accurate production with dependable customer support. High-speed forming lines help reduce dents, leaks, and uneven shapes. Skilled technicians still matter. They understand how metal temper affects filling-line performance.
Automated vision systems inspect printing, dimensions, and surface defects. Wall-thickness controls help keep can bodies consistent. However, automation is not perfect. Human investigation remains necessary when defects appear.
Request batch traceability, material records, pressure-test results, and defect rates. Ask for documented corrective actions after failures. Recent audit records are useful. A certificate alone proves little.
Look for verified data on recycled content, energy use, water use, and material losses. Recycled aluminum may use about 95% less energy than primary aluminum. Ask how the calculation was made. Different reporting boundaries can make comparisons misleading.
A lighter can can reduce material use and transport emissions. Excessive lightweighting may increase dents and filling-line problems. Test the can before making a decision. Lighter is not always better.
Test seam strength, coating resistance, print durability, and dimensional consistency. Run sample cans through the actual filling line. Watch for jams, dents, and slower movement. Small problems become expensive.
Review realistic lead times, peak-season capacity, minimum order quantities, and emergency plans. Check regional production capability and metal shortage preparation. A large annual output number may hide limited availability. Capacity needs context.
Sorting, baling, remelting, coatings, and inks all influence recovery quality. Collection systems vary widely by region. A strong can design cannot fix every recycling weakness. My first impression may be wrong.
The 2026 global Aluminum Can Packaging industry is defined by manufacturers that combine advanced production capabilities, consistent quality control, flexible customization, and reliable international supply networks. Leading companies use technologies such as high-speed forming, precision printing, lightweighting, automated inspection, and protective coating systems to produce durable cans for beverages, food, personal care, and other permitted consumer products. Their competitiveness also depends on efficient operations, responsive customer service, and the ability to meet different market requirements across North America, Europe, Asia-Pacific, the Middle East, Africa, and Latin America.
Sustainability is now central to can manufacturing, with greater attention placed on recycled aluminum, energy-efficient processes, waste reduction, responsible sourcing, and closed-loop recycling systems. When evaluating manufacturers worldwide, buyers should compare production capacity, material quality, certifications, environmental performance, tooling and design support, lead times, logistics capabilities, and communication standards. A well-rounded assessment helps companies select a dependable partner that can deliver safe, attractive, recyclable, and cost-effective packaging while supporting long-term business and environmental goals.